Leave Your Message
Choosing a Diffuser Cap for global sourcing requires more than comparing unit prices. The cap influences fragrance control, visual identity, shipping safety, and customer confidence. A well-designed closure can help reduce evaporation during long-distance transport. It can also create a smoother, more consistent opening experience.
David Luttenberger, Global Packaging Director at Mintel, has said, “Packaging is part of the consumer experience, not merely a container.” That observation fits diffuser products closely. The cap is often the first component customers touch. Its weight, threading, finish, and fit can quietly shape their judgment. For international buyers, these details become practical sourcing questions. Can the cap match different bottle necks? Will the material tolerate fragrance oils? Does the supplier control color consistency across production batches?
Small details matter.
Global sourcing may provide broader material choices, competitive manufacturing capacity, and access to specialized finishing techniques. Yet the lowest quotation can hide costly weaknesses. A cap may look excellent in a sample, then loosen during vibration testing. A coating may appear stable, then fade under warehouse heat. These risks deserve honest attention.
Experienced buyers should request dimensional drawings, material declarations, production samples, and documented quality checks. They should also test leakage, torque, odor compatibility, and packaging durability. Supplier communication matters just as much. Time-zone delays, unclear specifications, and changing mold conditions can disrupt an otherwise promising project.
There is no universally perfect Diffuser Cap. The right choice depends on the bottle, fragrance formula, market expectations, and delivery route. Careful sourcing turns an attractive component into a dependable product advantage.
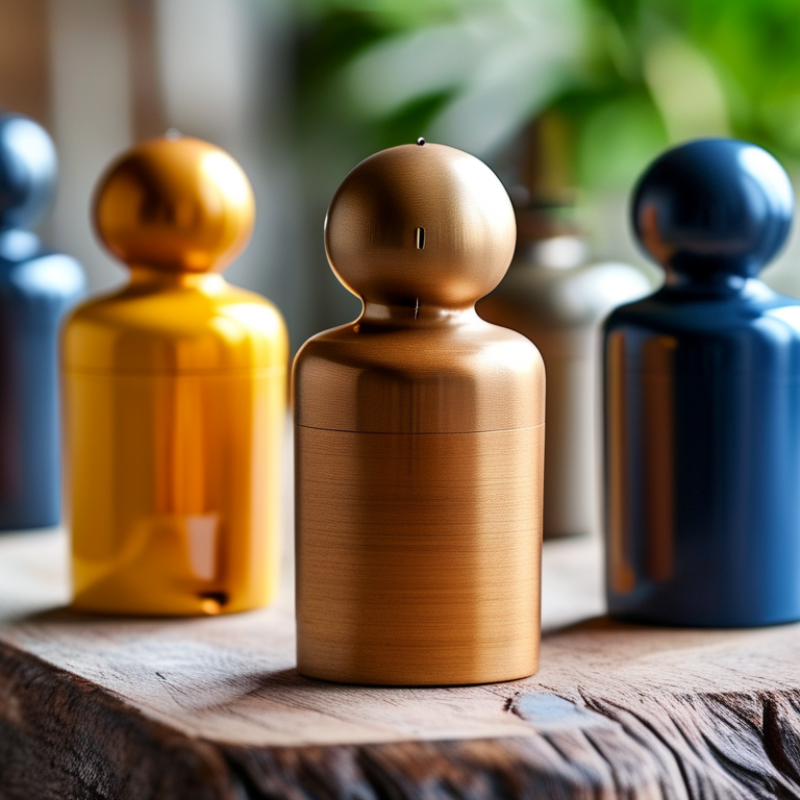
Choosing a diffuser cap for global sourcing requires more than comparing prices and appearance. The cap must manage evaporation, maintain a reliable seal, and support safe daily handling. In practical sourcing reviews, small design details often create large performance differences. A narrow outlet can slow liquid loss, while an overly tight closure may frustrate users.
Evaporation control depends on the cap’s opening, material, and internal airflow path. A well-designed diffuser cap releases fragrance gradually instead of flooding a room within minutes. The sealing surface should sit evenly against the container neck. It should also resist leakage during transport, storage, and temperature changes. Safety matters too. Rounded edges, stable fitting, and controlled release can reduce spills and accidental contact. However, laboratory results may not reflect every household condition. Humidity, heat, and rough handling still deserve attention.
Tips: Request samples from multiple suppliers and test them under realistic conditions. Check leakage after tilting, shaking, and storing the product for several days. Measure liquid loss over time. Ask for material specifications and quality-control records. Do not rely only on attractive prototypes. A cap may look precise but perform poorly after repeated use. Confirm dimensions with drawings, not assumptions. Local packaging requirements should also be reviewed before production.
| Function or Sourcing Dimension | Diffuser-Cap Configuration | How It Works | Relevant Materials or Dimensions | Global Sourcing Benefit | Recommended Verification |
|---|---|---|---|---|---|
| Evaporation control | Restricted-orifice diffuser insert | A small calibrated opening limits the exposed liquid surface and reduces the rate at which volatile liquid reaches the surrounding air. | Typical design variables include orifice diameter, insert height, liquid viscosity, and ambient temperature. Common cap polymers include polypropylene (PP) and high-density polyethylene (HDPE). | Helps control product consumption and improves consistency across different shipping and storage environments. | Measure mass loss over a defined time period at controlled temperature and humidity. Report the test liquid, fill level, cap torque, and storage orientation. |
| Evaporation control | Two-stage diffuser system | An inner insert regulates liquid release while an outer cap protects the insert during handling, storage, and transport. | Inner insert: PP, HDPE, or compatible elastomer. Outer cap: PP or HDPE. The insert and bottle neck must be designed as one compatible assembly. | Provides a practical balance between controlled diffusion, transport protection, and an attractive finished appearance. | Check diffusion rate, insert retention, cap removal force, and performance after vibration and temperature-cycle testing. |
| Sealing performance | Continuous liner or plug seal | A liner or internal plug creates a contact surface between the closure and the bottle finish, reducing liquid leakage and vapor escape. | Liner options may include foamed polymers, coated paperboard, PE, or elastomeric materials. Selection depends on the liquid formulation and required chemical resistance. | Supports cleaner international distribution and reduces the risk of leakage-related product loss. | Perform leak testing in upright, inverted, and horizontal positions. Inspect the seal after cap application and after transport simulation. |
| Thread compatibility | Screw cap matched to the bottle neck finish | Continuous internal threads engage with the matching external threads on the container neck. | Common neck-finish examples include 18-410, 20-410, 24-410, 28-410, and 33-400. The finish code must be confirmed with an actual neck drawing or physical sample. | Improves sourcing flexibility by allowing qualified suppliers to produce compatible components against a defined industry finish. | Confirm thread profile, pitch, height, neck outer diameter, land diameter, sealing surface, and application torque. Do not rely on nominal size alone. |
| Vapor sealing | Inner plug with compression fit | The plug presses against the inside of the container neck to create a secondary barrier beneath the external cap. | Usually produced from a chemically compatible polymer or elastomer. Compression must be controlled to avoid leakage without making assembly excessively difficult. | Provides additional protection for volatile formulations during long-distance shipping and warehouse storage. | Compare vapor-loss results with and without the plug. Check plug insertion depth, deformation, retention, and compatibility with the product. |
| Tamper evidence | Breakable ring or tear-band closure | A bridge-connected band separates or visibly breaks when the cap is opened for the first time. | Commonly molded from PP or HDPE. Ring dimensions and bridge strength must match the selected bottle finish and capping equipment. | Provides visible evidence of first opening without requiring a separate security component. | Verify complete ring separation, bridge break force, visual evidence after opening, and compatibility with automated capping lines. |
| Child-resistant packaging | Push-and-turn or squeeze-and-turn closure | The opening action requires coordinated movement that is intended to make access more difficult for young children while remaining usable by adults. | Usually manufactured from PP or HDPE with a compatible liner or plug. The final package, not only the cap, must be tested as an assembled system. | Supports safety-oriented sourcing for products that may require child-resistant packaging in the destination market. | Use an accredited laboratory to test the complete package against the applicable destination-market requirements, such as ISO 8317 or 16 CFR 1700.20 where relevant. |
| Material compatibility | Cap, liner, insert, and bottle selected as a matched system | Each material is evaluated for swelling, softening, cracking, discoloration, odor transfer, and loss of sealing force when exposed to the formulation. | PP and HDPE are widely used closure materials, but suitability depends on the chemical composition, concentration, temperature, and exposure time. Silicone and other elastomers require formulation-specific review. | Reduces quality variation when sourcing caps and bottles from different manufacturing locations. | Conduct compatibility testing with the actual formulation, including accelerated aging and post-exposure dimensional and sealing checks. |
| Application consistency | Torque-controlled screw closure | Specified application torque seats the cap and liner consistently without over-compressing the seal or damaging the threads. | Torque values are package-specific and depend on neck finish, liner type, thread design, and equipment. A universal torque value should not be assumed. | Improves repeatability between production batches and helps suppliers maintain the same closure performance. | Establish minimum and maximum application-torque limits through laboratory trials and confirm removal torque after storage and transport testing. |
| Transport protection | Protective overcap or recessed diffuser outlet | The outer geometry reduces direct contact with the diffuser outlet and helps prevent accidental impact during packing and handling. | The design should maintain clearance around the outlet while avoiding interference with cartons, dividers, and automated filling or capping equipment. | Can reduce outlet damage and contamination risks during international logistics. | Perform drop, vibration, compression, and temperature-cycle testing using the final filled package and shipping configuration. |
| Quality control for global sourcing | Defined dimensional and functional inspection plan | Critical dimensions and performance characteristics are documented so that different qualified suppliers can produce interchangeable parts. | Key inspection points include thread dimensions, cap height, liner presence, insert position, color, flash, cracks, burrs, and sealing performance. | Reduces supplier-to-supplier variation and simplifies incoming inspection across international purchasing locations. | Use approved drawings, control samples, measurable acceptance limits, batch traceability, and a documented inspection report for every production lot. |